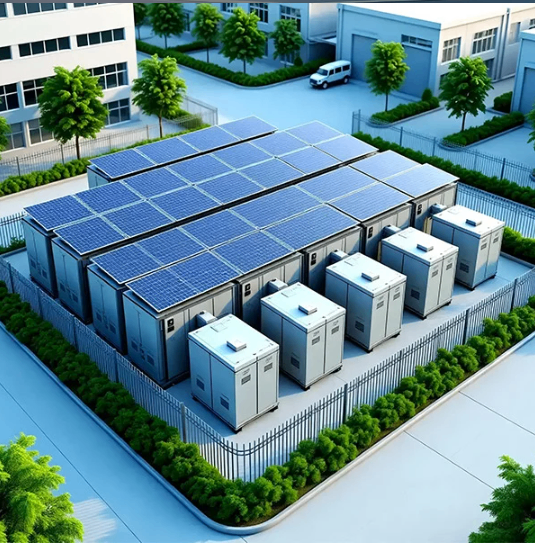
A battery energy storage system may arrive at an industrial facility with completed factory testing, documented specifications and installed safety equipment. That does not mean it is ready for normal operation.
Once the battery cabinets, power conversion equipment and electrical connections are installed, the entire system must be checked under the conditions of the actual project. Equipment that performed correctly during factory testing may behave differently after being connected to a factory's transformers, distribution boards and energy management platform.
This is where battery energy storage system commissioning becomes important.
Commissioning is not simply the moment when an operator switches on the battery. It is a controlled process of verifying that the installed equipment matches the approved design, that its components communicate correctly and that it can perform its intended functions safely.
For industrial facilities, the commissioning stage also establishes a reference for future maintenance. Without reliable initial records, it can be difficult to determine whether a performance issue developed during operation or existed before the system was handed over.
A practical commissioning plan should therefore address electrical installation, battery controls, functional testing, operating restrictions and documentation before the system enters regular service.
Why Is Factory Testing Not Enough for Industrial Battery Storage?
Manufacturers usually perform various inspections and tests before shipping energy storage equipment. These may include electrical checks, component verification, communication testing and selected functional tests.
Such testing provides evidence that equipment meets defined requirements under the conditions in which it was tested.
However, factory acceptance testing and site acceptance testing serve different purposes.
Factory acceptance testing, commonly called FAT, is performed before equipment delivery or installation. Its purpose is to verify specified equipment functions and identify manufacturing or configuration issues.
Site acceptance testing, often abbreviated as SAT, checks the equipment after it has been installed and integrated with the actual facility.
Consider a battery storage cabinet that passes factory testing. The cabinet may have correctly functioning sensors, internal protection devices and communication interfaces.
After delivery, the installer connects it to a power conversion system and a site-wide energy management system.
The complete installation now depends on additional components, including external electrical cables, protection equipment, communications networks and site-specific operating settings.
A communication error between the battery management system and the power conversion system may not have appeared during the original factory test.
Similarly, a metering configuration that works in a laboratory may require adjustment when connected to the facility's electrical distribution system.
These issues explain why project owners should not regard factory documentation as a substitute for on-site verification.
A useful distinction is shown below.
| Testing stage | Main objective | Typical verification |
|---|---|---|
| Factory acceptance testing | Confirm equipment meets defined factory specifications | Components, controls, selected functions |
| Installation inspection | Verify correct physical installation | Cabling, mounting, labeling and connections |
| Cold commissioning | Check suitable functions before main energization | Auxiliary systems, communication, protection readiness |
| Hot commissioning | Verify energized operation | Controlled startup, charging and discharging |
| Site acceptance testing | Demonstrate agreed system performance | Functional response, operating limits and test records |
| Operational handover | Transfer an accepted system to the operator | Documentation, training and unresolved item management |
The exact sequence varies by project. Some contracts use different names for individual acceptance stages.
What matters is that the scope, acceptance criteria and responsible parties are agreed before testing begins.
What Electrical Checks Are Needed Before the First Startup?
Before energizing an industrial battery system, qualified personnel need to confirm that the installation is consistent with the approved electrical design.
This stage involves more than checking whether all cables appear to be connected.
A battery storage installation may include DC battery circuits, AC power conversion equipment, transformers, circuit breakers, protective relays and auxiliary power supplies.
Each part must be checked according to the applicable commissioning procedure.
One important task is verifying equipment identification.
The installed battery cabinets, PCS units, meters and protection devices should match the approved drawings and equipment schedules.
Cable identification is also important. Incorrect labeling or undocumented changes can complicate both commissioning and later maintenance.
Grounding and bonding arrangements need verification to ensure that the installation meets the relevant electrical requirements.
Electrical connections should be inspected using the manufacturer's specified procedures. Where applicable, technicians should review connection torque records and approved electrical test results.
Insulation resistance and other electrical tests may also be required, but their suitability depends on the equipment and the manufacturer's instructions. Sensitive electronics and connected battery components must not be exposed to inappropriate test voltages.
The project team should also verify access to emergency isolation devices and confirm that electrical warning labels are installed correctly.
Physical inspection can reveal problems that are easy to overlook during construction.
Examples include unsupported cables, damaged cable insulation, blocked equipment access or environmental seals that were not completed correctly.
These defects should be documented and resolved according to their severity before the relevant commissioning stage proceeds.
An important principle is that a battery retains stored electrical energy even when disconnected from an external power supply.
Personnel must follow approved isolation procedures and should never assume that opening a switch makes every internal battery connection safe to touch.
Electrical commissioning is therefore a task for qualified professionals, not a routine user inspection.
How Can You Test BMS PCS and EMS Communication?
An industrial energy storage installation relies on several control systems working together.
The battery management system, or BMS, monitors conditions such as cell voltage, temperature, current and state of charge.
The power conversion system, or PCS, controls electrical energy conversion between the battery and the AC electrical network.
The energy management system, or EMS, may coordinate charging and discharging according to the facility's operating requirements.
Although these systems have different responsibilities, they need to exchange accurate information.
For example, the PCS may request battery discharge power. The BMS must communicate the permitted operating limits so that the request does not exceed the battery's allowable conditions.
The EMS may issue a schedule for charging during a particular period. The PCS then needs to respond according to its capabilities and the restrictions communicated by the BMS.
A communication fault can disrupt this coordination.
During commissioning, technicians should verify that devices are correctly identified and that the expected measurements are available.
Battery SOC, voltage, current, temperature and operating status should be checked for sensible values.
The team should also confirm that control commands reach the intended equipment and that the displayed results correspond with actual operating behavior.
Time synchronization deserves attention.
If the battery management system, PCS and energy management platform record events using inconsistent timestamps, troubleshooting becomes more difficult.
For example, a battery protection event may appear to occur after a PCS shutdown even though it actually triggered the shutdown.
Communication-loss behavior should also be tested through approved procedures.
A system should respond according to its documented control strategy when a communication link becomes unavailable.
This may involve restricting power, entering a defined operating state or initiating a protective shutdown.
The response depends on the equipment design and should not be improvised during commissioning.
For larger projects, technicians may also verify remote monitoring access and the accuracy of information displayed on the operator's interface.
Successful communication testing means more than seeing that every device is online. It means confirming that the complete control system exchanges the right information and responds correctly.
What Performance Tests Should Be Completed Before Handover?
Once installation checks and protection prerequisites have been satisfied, the project team can perform the approved energized tests.
These tests help determine whether the system can deliver the functions specified in the project agreement.
Controlled charging and discharging are common elements of the process.
The commissioning team may test whether the PCS follows permitted power commands, whether battery limits are respected and whether the system operates without unexpected interruptions.
Energy capacity testing may also be required.
However, capacity must be measured under clearly defined conditions.
The starting and ending state of charge, battery temperature, discharge power and measurement location can all influence the recorded result.
For example, energy measured at the battery's DC terminals is not the same as energy delivered through the PCS to the facility's AC network.
Conversion losses and auxiliary equipment consumption affect the relationship between these values.
A project acceptance test should therefore specify the exact measurement boundary.
The same principle applies to round-trip efficiency.
Round-trip efficiency compares the useful energy recovered from the system with the energy supplied during charging, under a defined test procedure.
The result depends on operating power, temperature, measurement boundaries and auxiliary consumption.
A test conducted under one set of conditions should not automatically be compared with a manufacturer's figure measured under different conditions.
The following table identifies several common commissioning measurements.
| Test item | What should be verified | Important consideration |
|---|---|---|
| Charging operation | Battery accepts controlled charging commands | SOC and temperature restrictions |
| Discharging operation | System delivers approved output power | PCS and battery power limits |
| Usable energy | Energy delivered within defined operating limits | Test temperature and measurement boundary |
| Round-trip efficiency | Energy recovered relative to charging energy | Conversion and auxiliary losses |
| BMS protection | Appropriate response to defined test conditions | Approved, non-destructive test procedures |
| EMS dispatch | Power commands and schedules operate correctly | Metering and communications |
| System alarms | Faults are recorded and reported | Alarm logic and timestamps |
| Restart behavior | Equipment follows the approved recovery sequence | Site-specific operational requirements |
Not every test must be performed by creating a real hazardous condition.
Protection functions should be verified using manufacturer-approved procedures, simulations or suitable test interfaces where applicable.
Testing should not deliberately expose battery cells to damaging conditions simply to demonstrate that protective equipment responds.
The acceptance values must come from the project contract, approved technical specifications and relevant test procedures.
If a system does not meet an agreed requirement, the result should be documented and the cause investigated before acceptance.
What Problems Commonly Delay BESS Site Acceptance?
A battery storage system can be mechanically complete while still having unresolved commissioning issues.
One common problem involves inconsistent equipment settings.
The BMS, PCS and EMS may have different versions of operating limits or communication configurations. Each device may work independently, but the complete system cannot follow the intended charging schedule.
Another issue involves meter placement or configuration.
An EMS may need to distinguish factory consumption from battery charging power and utility grid exchange.
If the required measurements are incorrectly configured, the controller may make decisions using inaccurate information.
Some sites also encounter differences between approved drawings and the final installed arrangement.
Changes to cable routes, protection devices or connection points may have occurred during construction without being fully reflected in the documentation.
These changes need to be reviewed because they can affect testing and future maintenance.
Alarm handling is another area where difficulties appear.
A system may report an abnormal condition correctly but fail to display enough information for an operator to understand what happened.
In other cases, a fault may be recorded locally but not transmitted to the remote monitoring platform.
A commissioning team should verify that important alerts are visible through the required operating interfaces.
Environmental control equipment can also affect acceptance.
For example, a battery cabinet's cooling equipment may operate normally during basic startup but show unexpected behavior during sustained charging or discharging.
This is why representative operating tests are valuable.
The project team should maintain a documented list of unresolved items, sometimes called a punch list.
Each item should include a clear description, responsible party, corrective action and verification status.
Safety-critical deficiencies should be resolved before the affected equipment is placed into operation.
Other items should be handled according to the agreed acceptance procedure, with clearly documented responsibilities.
Simply marking a test as completed is not enough. The results and any exceptions should be traceable.
What Documents Should an Industrial Battery Supplier Provide at Handover?
Commissioning is complete only when the project owner has the information needed to operate and maintain the accepted system.
The handover package should reflect the equipment that was actually installed, not merely the original design proposal.
As-built electrical drawings are particularly important.
They identify the completed connections, equipment locations and relevant configuration details.
The owner should also receive applicable operating manuals, maintenance instructions, equipment specifications and verified settings.
A commissioning report should record which tests were performed, the conditions under which they were conducted and the results.
Where acceptance criteria apply, the report should show whether those criteria were satisfied.
Relevant alarms, corrective actions and final verification records should be included.
Operator training is another essential part of handover.
Facility personnel need to understand normal operating modes, monitoring interfaces, routine responsibilities and the procedure for reporting abnormal conditions.
They should also know which activities require assistance from the manufacturer or qualified service personnel.
Remote monitoring permissions and software access need to be transferred in a controlled manner.
The owner should understand how operating records will be retained and who is responsible for software maintenance and technical support.
A useful handover package may include the following:
-
Final electrical drawings and equipment identification records.
-
Factory and site acceptance documentation.
-
Commissioning test procedures and recorded results.
-
Approved operating parameters and configuration information.
-
Maintenance instructions and inspection schedules.
-
Emergency response and shutdown information.
-
Warranty documents and technical support arrangements.
-
Operator training records and unresolved item documentation.
This information becomes particularly valuable several years later.
If the battery begins delivering less energy than expected, its original acceptance records provide a starting point for comparison.
If equipment settings are changed, the commissioning configuration can help identify what has been modified.
If a component needs replacement, accurate drawings and equipment records make the work easier to plan.
For industrial buyers considering an industrial energy storage system, commissioning and handover requirements should be included in the procurement discussion rather than treated as paperwork after installation.
A correctly designed battery system needs to function as part of the facility's electrical infrastructure. That performance must be demonstrated through documented testing and supported by reliable operating information.
The successful delivery of an industrial battery storage project is not defined by the first time the system produces power. It is defined by whether the installed equipment has been verified, accepted and transferred to the operator with a clear understanding of how it should perform.




Reviews
There are no reviews yet.